
Turning on CNC Sliding-Headstock Lathes
SABNER uses CNC sliding-headstock lathes for the series production of small precision parts manufactured to customer specifications. The typical production range includes diameters of Ø0.5–12 mm, lengths of 1–150 mm, and annual demand starting at 10,000 pieces per component.
This technology, also known as Swiss-type turning, combines the machining of bar stock with stable workpiece guidance close to the cutting zone. This makes it particularly suitable for the series production of small parts and slender components, where the method of supporting the material is critical to process stability.
SABNER focuses on CNC turning. We do not offer CNC milling as a separate service. If the part’s geometry requires additional operations that can be performed as part of the process on a CNC lathe, we evaluate their feasibility on a case-by-case basis using the project documentation.
What is a CNC sliding-headstock lathe?
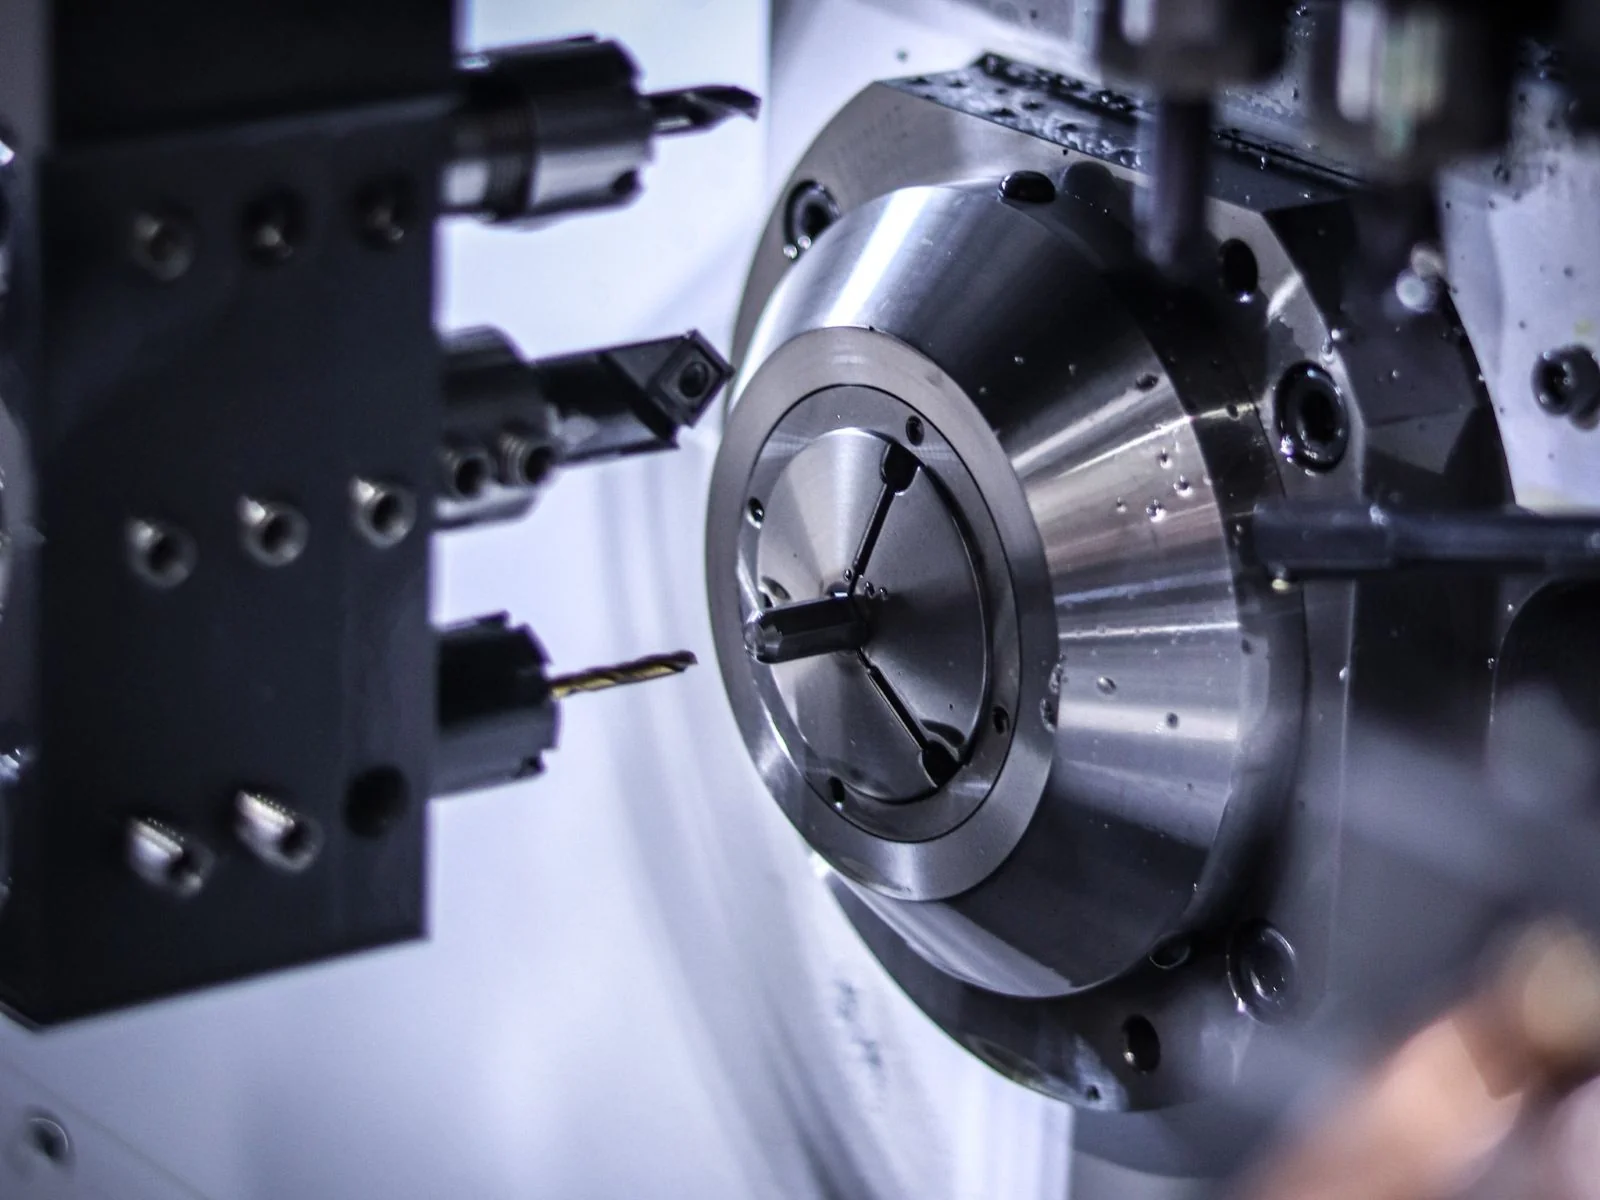
A CNC sliding-headstock lathe is a lathe in which the bar stock moves axially with the moving headstock relative to the tooling. In a typical Swiss-type configuration, the bar passes through a guide bushing located very close to the cutting zone.
This design limits the free overhang of the material where the tool is operating. The guide bushing supports the bar close to the machining point, thereby reducing its deflection and susceptibility to vibration. This is particularly important when machining long, slender parts with small diameters.
The terms sliding-headstock automatic lathe, sliding-head lathe, Swiss-type automatic lathe, and Swiss-type lathe all refer to the same family of technologies. However, the specific machine configuration may vary depending on the type of part being produced.
When does turning on sliding-headstock lathes make sense?
This technology is particularly useful in the series production of small turned parts from bar stock, especially when the component’s geometry requires stable material guidance close to the cutting zone.
Good candidates include, among others, small-diameter parts and slender components whose length is large relative to their diameter. Limiting the material overhang helps maintain more stable machining conditions in such cases.
Production volume is also a factor. Once the process is set up, a sliding-headstock automatic lathe can repeat the same cycle for successive components, which is why this technology is well suited to the requirements of repeatable series production.
However, not every small part needs to be machined on a sliding-headstock lathe. The choice of technology is determined by a combination of geometry, material, drawing requirements, and planned volume. SABNER evaluates these factors before confirming the feasibility of a project.
How does a Swiss-type lathe support precision turning?
When machining a slender bar, the forces acting on it can cause deflection or vibration. The greater the free overhang of the material relative to its diameter, the more important proper support becomes.
This is particularly important in the production of small and slender parts. The design of a sliding-headstock lathe therefore allows specific geometries to be produced in a way that is better suited to their proportions than on a conventional lathe.
However, the machine’s design alone does not automatically guarantee a specific tolerance. The accuracy of a particular part also depends on its geometry, material, drawing requirements, tools, and the defined manufacturing process. We confirm the feasibility of producing a part after analyzing its documentation.
Production from Bar Stock and Series Automation
Sliding-headstock automatic lathes are designed to work with bar stock. The material is automatically fed into the machining zone, so once the process is set up, subsequent parts can be produced without manually clamping a separate blank for each piece.
In series production, it is not only important to produce a single correct part, but above all to repeat the prepared process throughout the entire production batch.
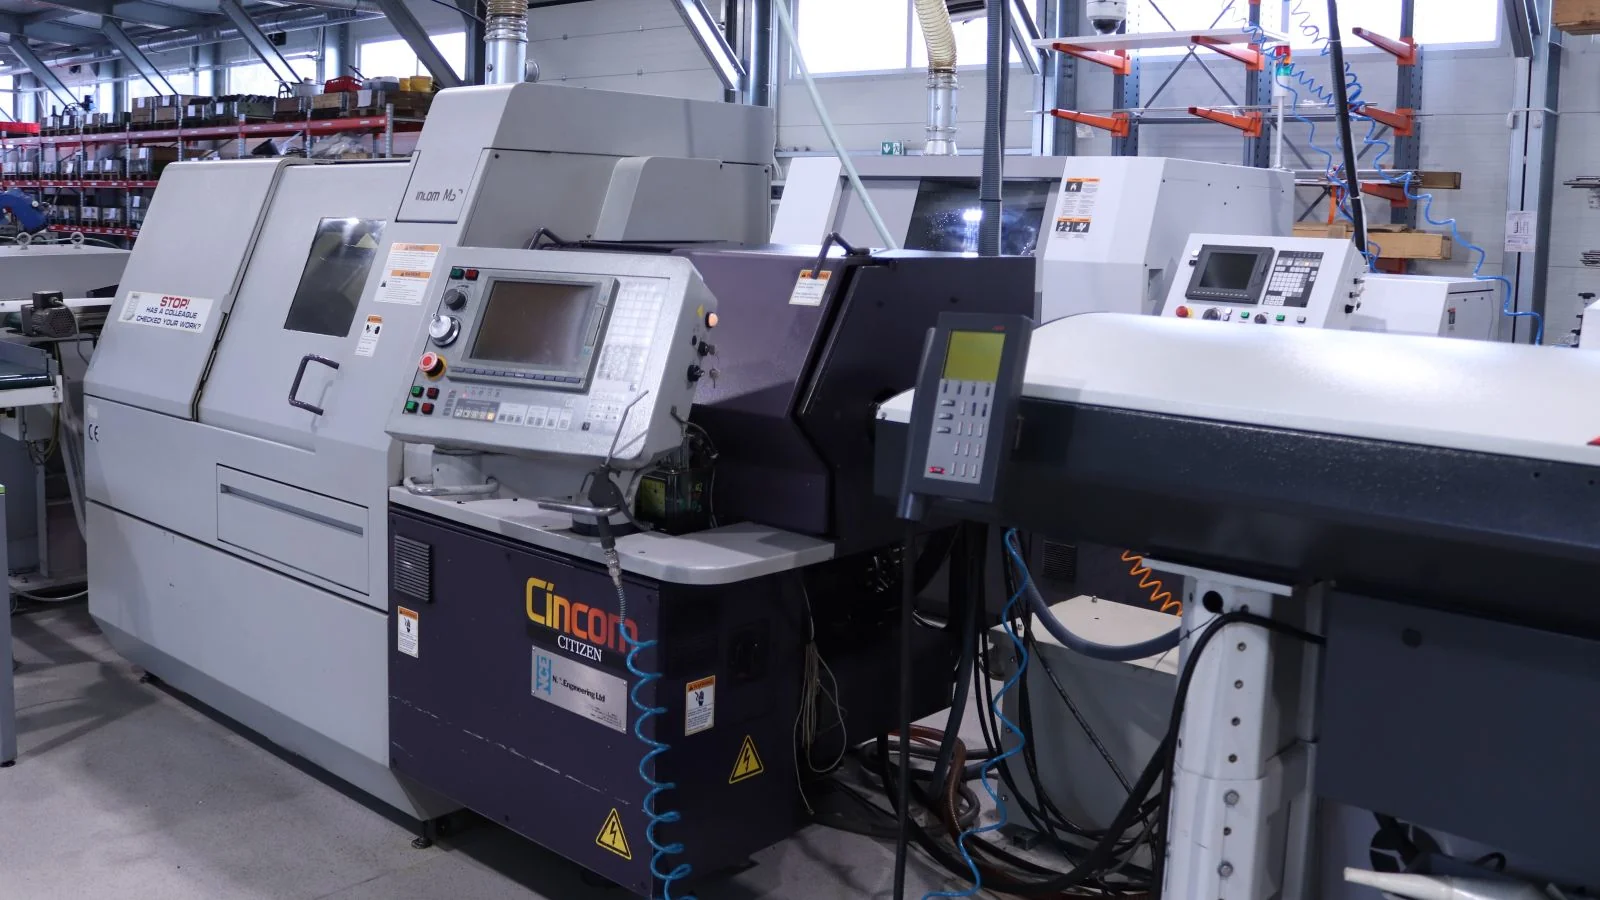
At SABNER, material feeding is also combined with the automatic removal of finished parts from the machine. Once the cycle is complete, the part leaves the machining zone without the need to remove each individual piece manually. This supports the process continuity characteristic of series production on automatic lathes.
Automation does not mean a lack of control over production. Its purpose is to ensure a repeatable method of executing successive cycles in accordance with the prepared program and manufacturing process.
The minimum requirement for a project to qualify at SABNER is 10,000 pieces per year per component. At higher annual volumes, the cost of process setup can be spread across a larger number of parts, which typically improves the economics of series production.
If a project requires prior validation of the proposed solution, samples or a small batch can serve as a validation stage before the main series production run. These are not offered as standalone prototyping or short-run production services.
What types of parts are suitable for sliding-headstock turning?
This technology is primarily used for small parts made from bar stock. Axial components are a natural application, but modern CNC lathes also allow more complex geometries to be produced within a prepared manufacturing process.
Whether a specific part is suitable for this technology depends, among other factors, on the part’s diameter and length, the length-to-diameter ratio, the arrangement of geometric features, the material, and the batch size.
SABNER uses sliding-headstock lathes to manufacture small precision parts according to customer specifications. We do not offer a standard product catalog. Each component is manufactured to a specific drawing, model, or project specification.
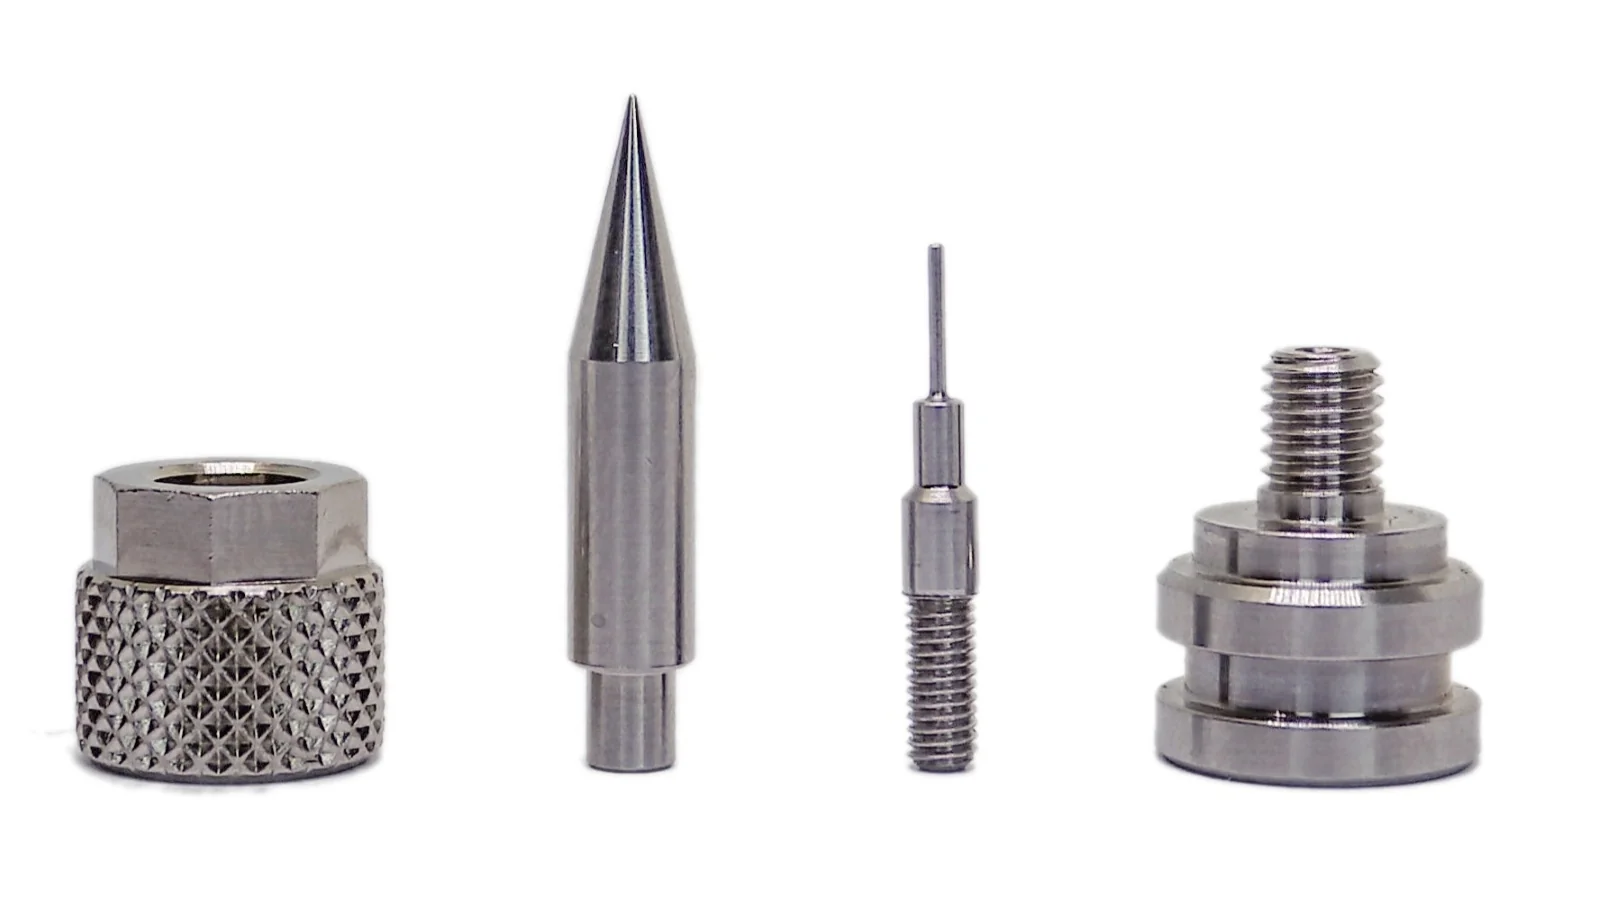
Typical part categories include, among others, turned parts, pins, inserts, fittings, and custom technical components, provided their geometry, material, and production requirements align with SABNER’s manufacturing capabilities.
What materials do we machine?
For the series production of small turned parts, SABNER most frequently uses stainless steel, titanium, and brass. These are the main material groups in the company’s current production profile.
Depending on project requirements, we also evaluate aluminum, free-cutting steels, structural steels, and selected specialty materials, including materials from the Inconel family and other alloys requiring a customized manufacturing approach.
Material selection influences how the process is prepared; therefore, we confirm the feasibility of series production for a specific part based on the material grade, part geometry, and documentation requirements.
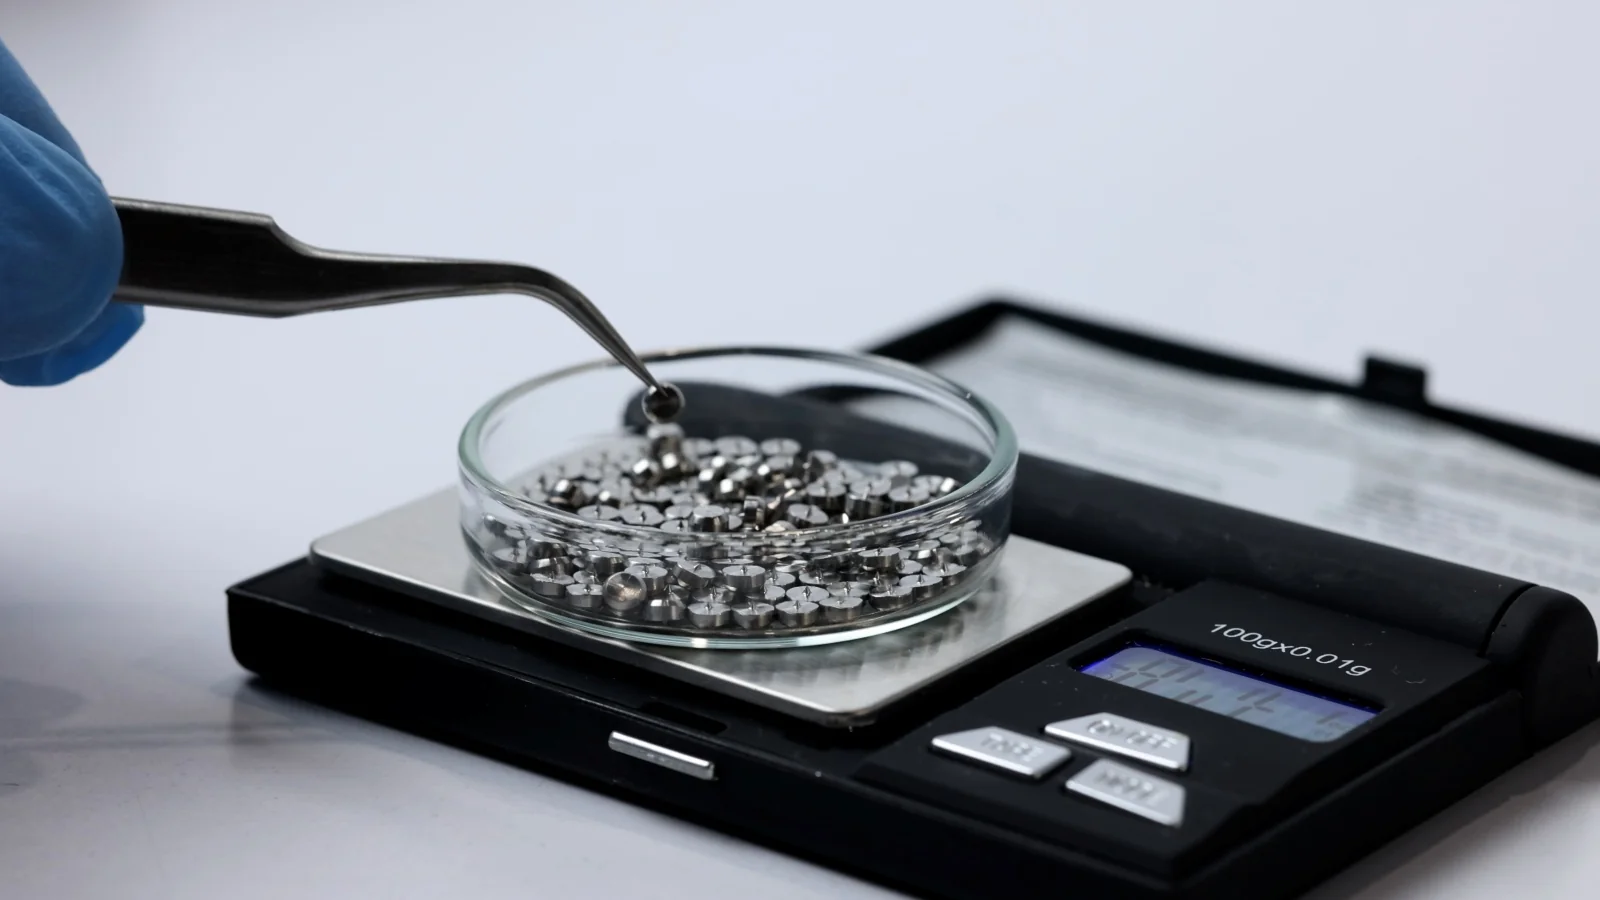
Scope of CNC Sliding-Headstock Turning at SABNER
SABNER focuses on the series production of small CNC-turned parts. A typical project scope includes:
| Parameter | SABNER’s Scope |
|---|---|
| Part diameter | Ø0.5–12 mm |
| Part length | 1–150 mm |
| Annual demand | at least 10,000 units per component |
| Basis for production | customer documentation and requirements |
| Samples | possible as part of the validation phase for a series-production project |
Meeting the basic dimensional and volume parameters is the first stage of qualification. The final feasibility of producing a part also depends on the geometry, material, and quality requirements specified in the documentation.
Tolerances, production conditions, and price are determined for a specific project after analyzing its requirements. As a result, the quotation details are based on the actual geometry and production conditions rather than on the general capabilities of a machine-tool class.
Sliding-Headstock Lathes and Precision CNC Turning in Series Production
Sliding-headstock lathes are one of the technologies used in precision CNC turning for series production. They are particularly important when the part is small or slender, is machined from bar stock, and requires stable material support near the cutting zone.
A comprehensive precision CNC turning service for series production also includes project qualification, process preparation, quality requirements, and the organization of series production. Selecting a Swiss-type lathe is therefore part of the technological decision made for a specific component rather than a separate project objective.
If you are unsure whether a part is best manufactured using Swiss-type technology, please submit your documentation for analysis. Based on the documentation, we can assess the appropriate manufacturing method.
What should you submit for project evaluation?
The best starting point is the documentation defining the part. It allows us to evaluate not only the basic dimensions but also the geometric features and requirements that influence the choice of technology.
We recommend including the following with your inquiry:
- technical drawing or 3D model
- material information
- planned annual demand
- additional quality or technical requirements relevant to the project
SABNER focuses on series production; therefore, the basic qualification threshold is a minimum of 10,000 units per year per component.
If the project requires prior validation, samples may be considered as a preliminary stage before the main production run. The goal is to prepare and validate a solution intended for repeatable series production.
Based on the data you provide, we can assess how well the project aligns with SABNER’s manufacturing profile and determine the next stage of collaboration.
Frequently Asked Questions About CNC Sliding-Headstock Turning
What does “Swiss-type” turning mean?
Swiss-type turning refers to a turning process using a lathe with a moving headstock. In a typical configuration, the bar stock is guided through a guide bushing located close to the cutting zone, which limits its free overhang during machining.
How does a Swiss-type lathe differ from a standard CNC lathe?
The most important difference concerns how the material moves and is supported. In a Swiss-type lathe, the bar moves axially with the sliding headstock relative to the tools and, in a typical Swiss-type configuration, is additionally guided through a guide bushing located close to the machining area.
What parts are best suited to sliding-headstock turning?
This technology is particularly well suited to small turned parts and slender components for which stable material guidance close to the cutting zone is advantageous. However, selecting the right process for a specific component requires an analysis of its technical documentation.
Are sliding-headstock automatic lathes suitable for series production?
Yes. Machining from bar stock, automatic material feeding, and automatic removal of finished parts enable the prepared cycle to be repeated for subsequent parts. SABNER uses this technology in series production projects starting at 10,000 units per year per component.
What materials can be machined on sliding-headstock automatic lathes?
At SABNER, the main material groups are stainless steel, titanium, and brass. Depending on the project, aluminum, free-cutting and structural steels, as well as selected specialty materials, are also evaluated.
What information should be provided for a production assessment?
The most important information includes part documentation, material, planned volume, and project requirements. Based on this information, we can assess whether the component falls within SABNER’s production scope and whether a sliding-headstock lathe is the appropriate solution.
Inquire About Series Production of Parts on Sliding-Headstock Automatic Lathes
If the project involves series production of small precision-turned parts, please submit the component documentation, material information, and planned annual demand.
SABNER typically carries out projects within the range of Ø0.5–12 mm, with part lengths of 1–150 mm and a minimum demand of 10,000 pieces per year per component. After analyzing the documentation, we can assess whether a CNC sliding-headstock lathe is the right technology for the part and determine the next steps for implementation.